Featured Wholesale & OEM Product Lineup
Direct factory supply with certified tonewood selection, strict acoustic quality control, and flexible MOQ options for international importers and distributors.

Wholesale 40" Cutaway Beginner Acoustic Guitars (AF-H00LC)
Engineered for entry-level learning programs and high-volume retail. Features a responsive spruce top, ergonomic cutaway body, and stable tuning machinery.
View Details
Ready to Ship 40" Student Cutaway Acoustic Electric Guitar (AF238CE)
Equipped with active under-saddle piezo pickup and 3-band EQ. Ideal for school bands and gigging students requiring stage-ready amplification.
View Details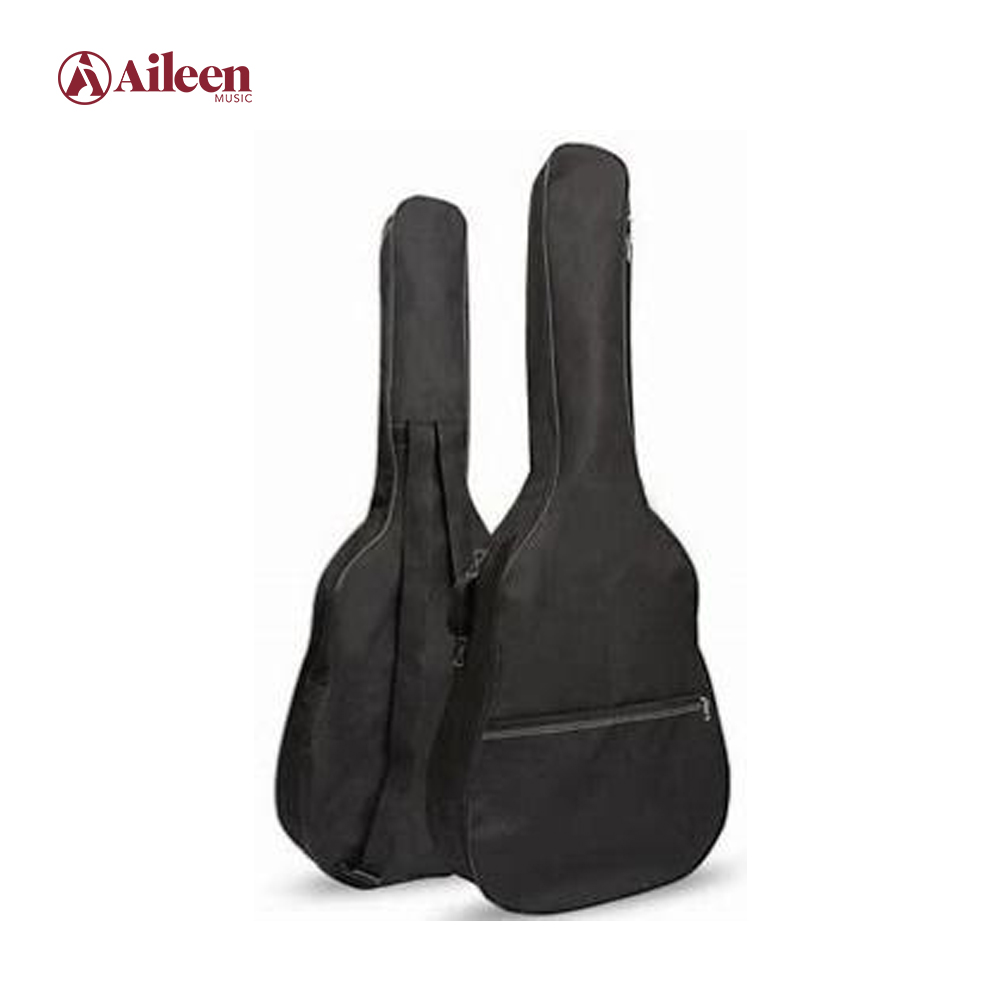
BGG602 36''-41'' 600D Oxford Cover Classical/Acoustic Soft Guitar Bag
Heavy-duty water-resistant oxford fabric with high-density padding, reinforced dual shoulder straps, and spacious accessory pockets for total gig protection.
View Details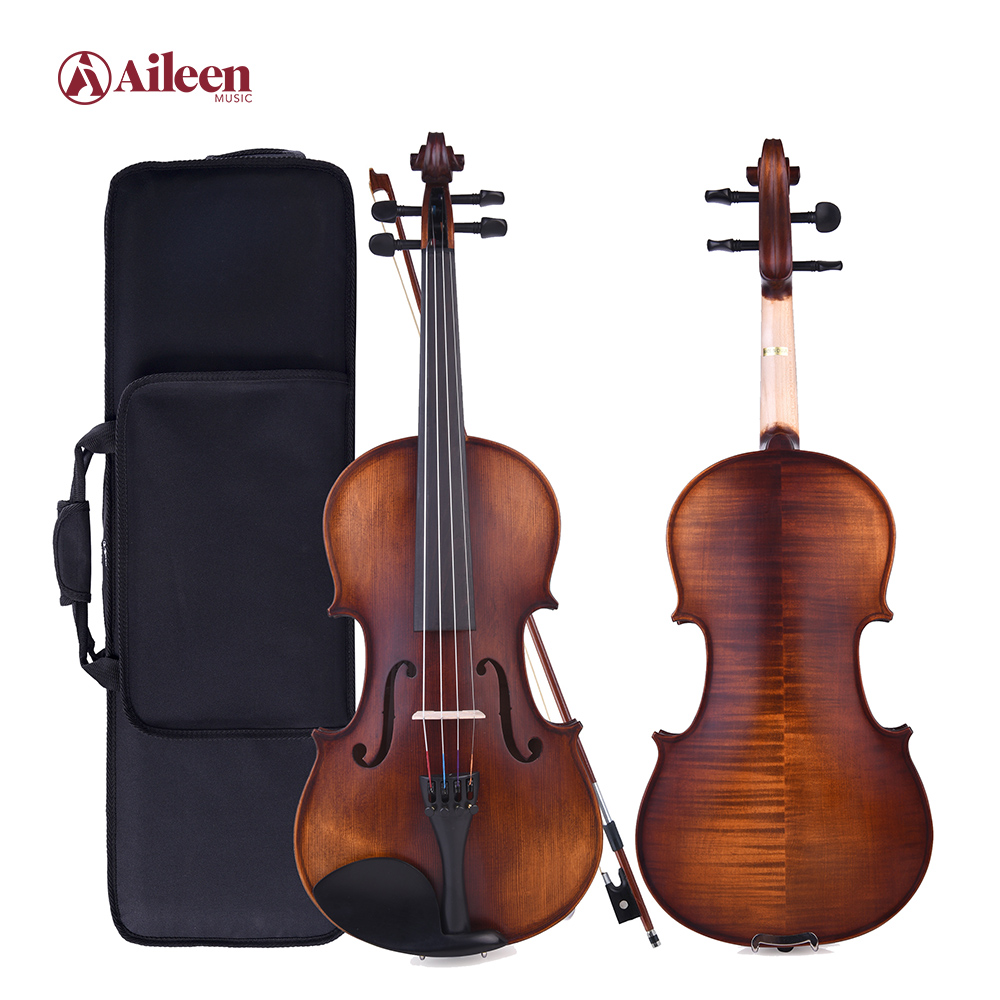
VM100 Selected Solid Spruce Top 4/4-1/16 Moderate Violin Set
Hand-carved solid spruce top with naturally aged maple back and sides. Includes ebony pegs, composite tailpiece with fine tuners, bow, and case.
View Details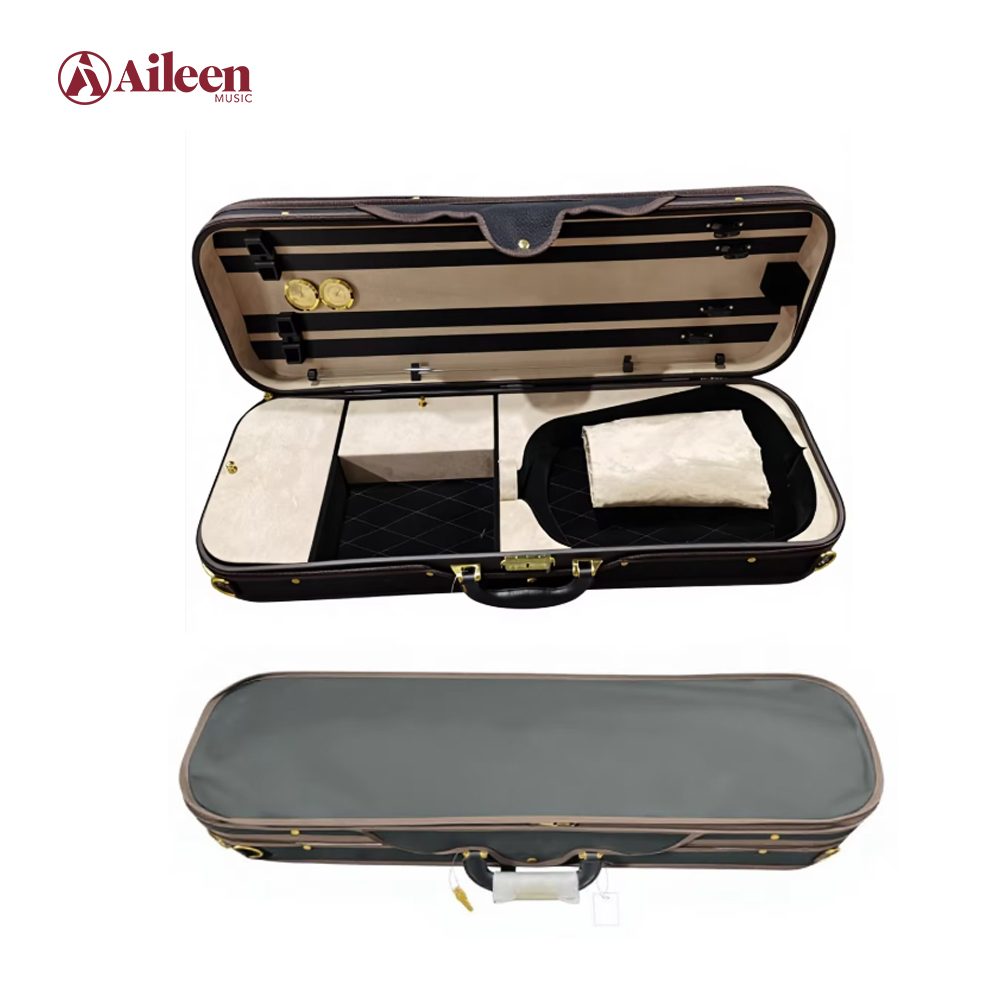
Aileen Stock Oblong Shape Deluxe Wooden Violin Case (CSV1067)
Professional multi-ply wooden shell with velvet interior, hygrometer humidity gauge, dual bow holders, and blanket cover for master instrument protection.
View Details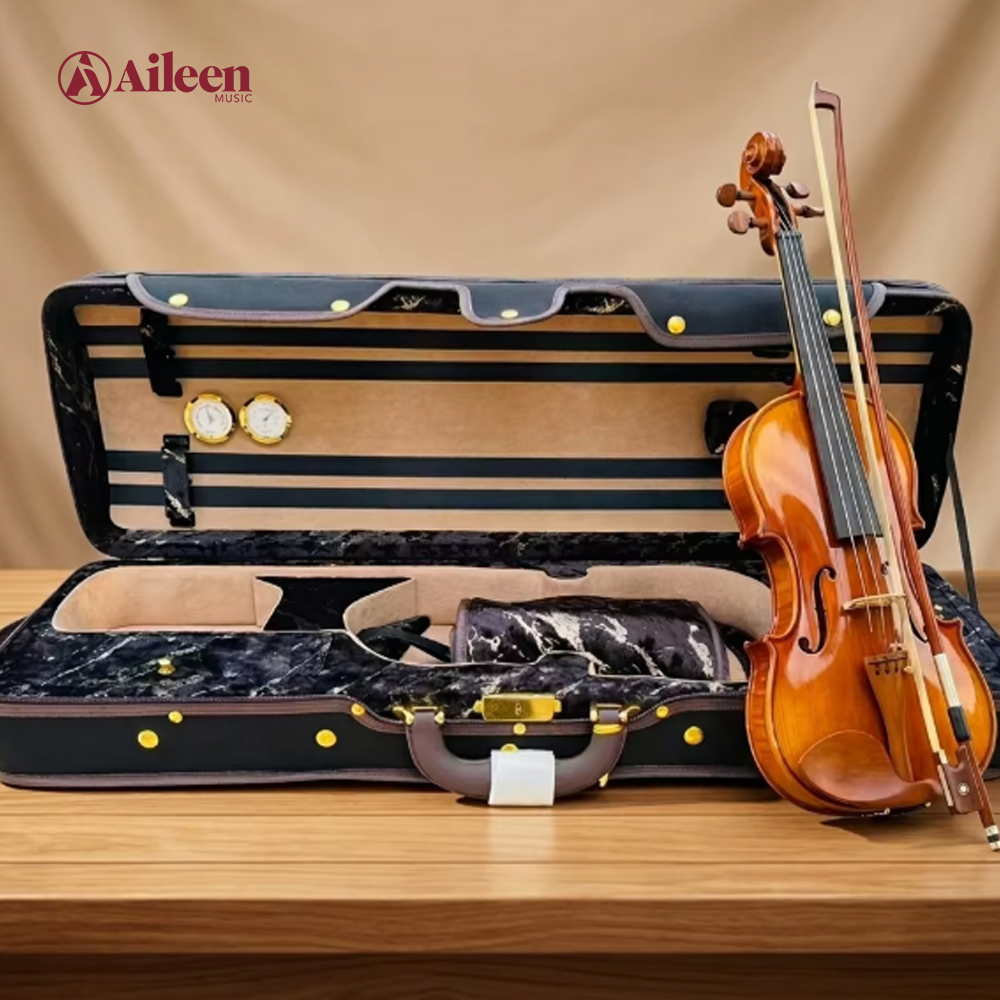
AileenMusic Oblong 4/4 Deluxe Foamed Violin Light Case CSV071A3
Ultra-lightweight shock-absorbing EPS hard foam core wrapped in durable nylon canvas. Perfect for students requiring daily transport resilience.
View Details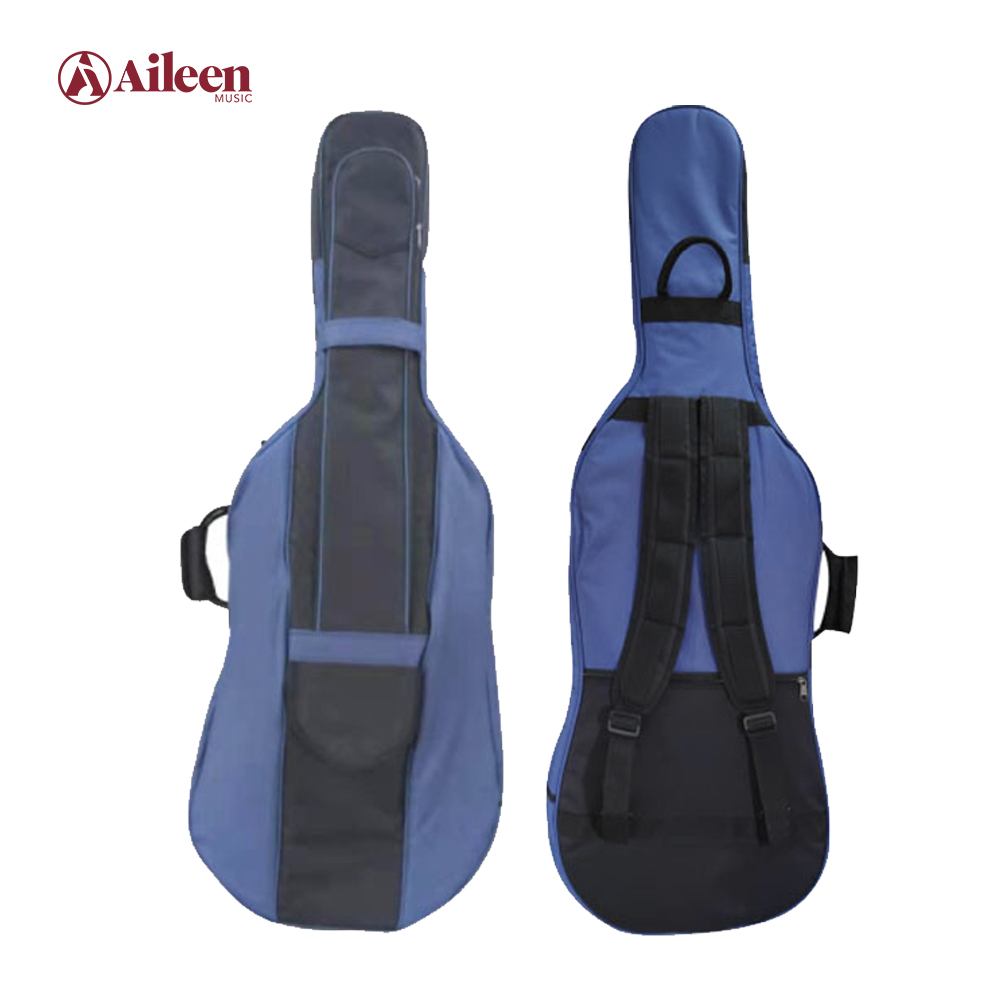
BGC014H 20mm Thick Padding Soft Carrying Cello Bag (4/4-1/16)
Heavy-duty 20mm foam interior cushioning, bridge support pad, bow pocket, and multi-point grab handles designed for orchestra instrument mobility.
View Details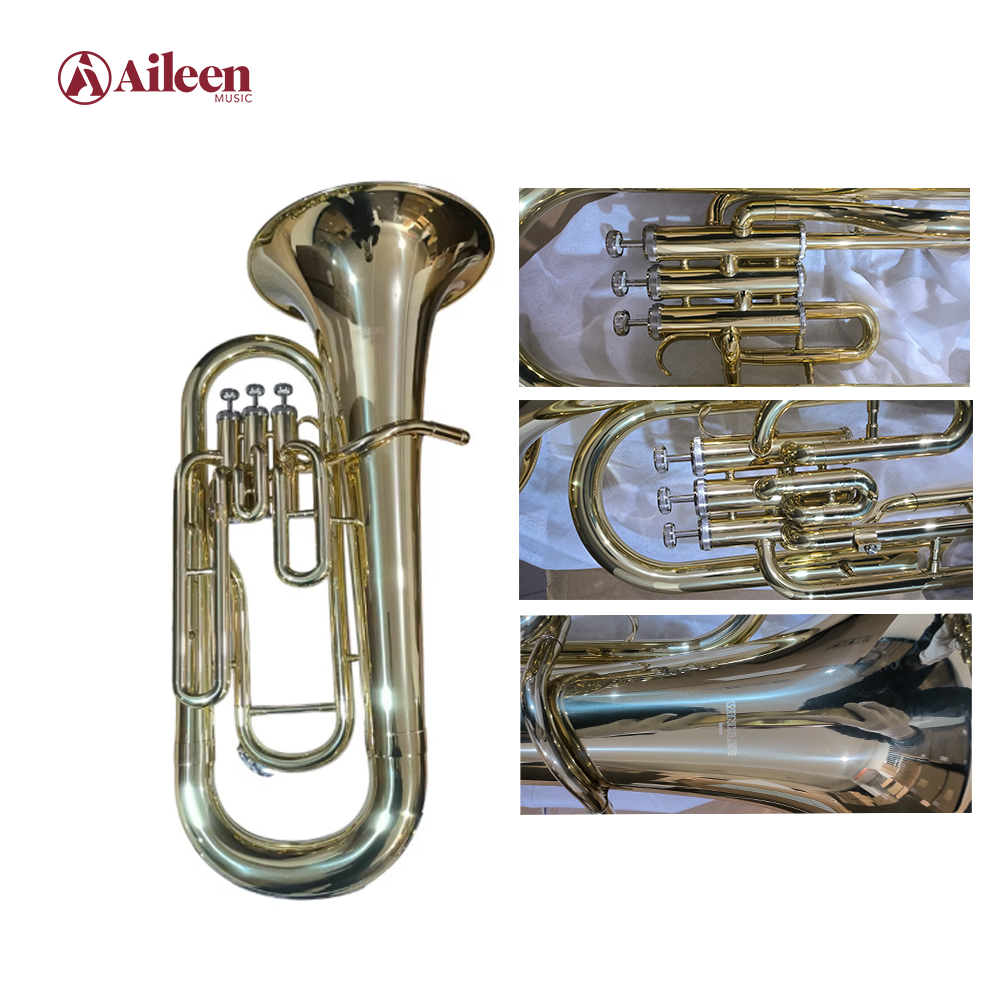
EU-G3400G Entry Level Student Yellow Brass Euphonium with Case
Precision-drawn yellow brass body with smooth cupronickel tuning slides. Delivers warm, resonant projection suited for school brass bands and ensembles.
View DetailsProven Manufacturing Footprint & Global Benchmark
Quantifiable excellence across three decades of international OEM/ODM B2B instrument export.
Global OEM Guitar Manufacturing: Executive B2B Procurement Strategy
In the highly competitive musical instrument market, global brand owners, chain retailers, and educational distributors face increasing pressure regarding supply chain integrity, tonewood stability, price-to-quality ratios, and private-label agility. Sourcing from a premier custom OEM guitar wholesale manufacturer requires moving beyond simple transactional pricing to evaluating factory engineering workflows, climate-controlled lumber seasoning, automated CNC machining accuracy, and international trade compliance standards (such as CITES regulations for protected timber species).
As a leading Chinese manufacturing conglomerate established in 1993, Chive Music Co., Ltd. (operating premier commercial brands including Winzz, Lexington, and Chive) has transformed B2B instrument manufacturing. Ranked No. 195 in the prestigious Music Trades Global 225, our production infrastructure integrates automated woodworking machinery with hand-lutherie craftsmanship to deliver scalable, defect-free guitar production for global partners.
The primary cause of warranty claims in imported acoustic and electric guitars is wood movement caused by inadequate moisture conditioning. Professional OEM guitar factories must maintain strict kiln-drying protocols, reducing timber equilibrium moisture content (EMC) to 8%–10% before CNC roughing, followed by mandatory stabilization periods in humidity-controlled conditioning chambers (45%–55% RH) prior to final neck setting and finish application.
Technical Comparison: Manufacturing Architecture Standards
Understanding the architectural distinction between entry-level volume manufacturing and advanced OEM specification levels is essential for procurement directors optimizing their brand portfolio:
| Specification Vector | Standard Entry-Level OEM | Professional Mid-Tier OEM | Master & Custom Shop OEM |
|---|---|---|---|
| Soundboard Wood | Laminated Linden / Agathis | Solid Sitka Spruce / AAA Mahogany | Torrefied Solid Engelmann / Cedar |
| Neck Construction | Multi-piece Okoume / Maple | 1-Piece Mahogany with Dovetail Joint | Quarter-Sawn Flame Maple with Carbon Rods |
| Fretboard Finish | Engineered Tech-Wood | Select Indian Rosewood / Ebony | Grade-A African Ebony with Bound Edges |
| Drying Cycle | Standard Air Dry (15–20 days) | Kiln Dried + 60-day Chamber Cure | Thermally Modified (Roasted) + Natural Aging |
| Finish Cure System | Air-Dried Nitro/Poly (Thick coat) | High-Gloss Polyurethane (Ultra-thin) | Thin UV-Cured Resin or Hand-Rubbed Oil |
Future Guitar Procurement & Manufacturing Trends (2025–2030)
Key industry shifts shaping product development, material selection, and factory sourcing for international music brands.
1. Thermal Modification (Torrefaction)
Torrefied (roasted) tonewood tops and necks heat timber in an oxygen-free kiln above 200°C. This artificial aging process crystallizes wood resins, resulting in vintage acoustic resonance, structural immunity to climate changes, and enhanced neck stability across international shipping zones.
2. CITES-Compliant Eco Tonewoods
Stricter global forestry oversight is accelerating the replacement of rosewood with eco-friendly alternatives such as thermally stabilized Jatoba, Laurel, and Richlite engineered fingerboards. Forward-thinking OEM buyers are adopting certified sustainable top woods without sacrificing acoustic energy transmission.
3. Headless & Ergonomic Guitars
Modern players increasingly favor headless electric guitars, multi-scale fanned fretboards, and lightweight body contours. These designs require high-precision multi-axis CNC routing and specialized headless bridge hardwares—technologies fully implemented across our Winzz Orbit and Headless production lines.
4. Smart Electronics & Onboard DSP
Acoustic-electric models are expanding beyond basic piezos to feature integrated digital signal processors (DSP), impulse response (IR) modeling, reverb/delay FX without external amps, and Bluetooth connectivity for app-based practicing, driving modern consumer demand.
5. Environmentally Friendly UV Coatings
Automated UV-cured acrylic and polyurethane coating systems cure instantly under ultra-violet lamps. This process eliminates volatile organic compounds (VOCs), produces ultra-thin finish coats that enhance natural top resonance, and reduces factory lead times by up to 14 days.
6. Consolidated Multi-Category Shipments
Distributors are mitigating rising container shipping costs by consolidating fretted instruments, orchestral strings, band brass, percussion, and gig bags into unified full-container loads (FCL) from single multi-category manufacturing hubs.
13-Stage Quality Controlled Manufacturing Assurance
To ensure total reliability across international supply chains, Chive Music Co., Ltd. operates a strictly audited 13-stage manufacturing process. Every instrument moving through our production facilities in Nanjing, Jiangsu, undergoes step-by-step verification overseen by our 79 skilled instrument specialists and ISO 9001 certified quality controllers.
Phase 1: Wood Selection & Machining
Kiln-dried tonewood blocks undergo precision moisture inspection prior to automated computer-numerical-control (CNC) routing for neck shaping, body profiling, and soundboard bracing. Drilling and grinding machines ensure sub-millimeter tolerances on neck-pocket joints and fret slots.
Phase 2: Finishing & Controlled Curing
Instruments pass through dust-controlled automated spray rooms for multi-coat lacquer application, followed by dedicated curing and drying chambers. Precision surface sanding between coats guarantees deep gloss optical clarity and smooth neck movement.
Phase 3: Fitting, Electronics & Setup
Hand-assembly teams press frets, dress fret ends to prevent sharp edges, install tuning machinery, and wire electronic components. Experienced luthiers cut nut slots, adjust bridge saddle heights, set truss rod relief, and conduct acoustic play-testing.
Phase 4: Inspection & Export Packaging
100% final quality checklist verification covering finish aesthetics, fret leveling, electronic noise floor, and intonation accuracy. Finished instruments are packed into humidity-sealed polybags and heavy-duty 5-ply double-wall export cartons.
Enterprise Credentials & Verification
Distributors and OEM brand partners gain competitive confidence through our certified track record and regulatory compliance:
- NAMM Permanent Member: Continuous active membership in the National Association of Music Merchants since 2003.
- ISO 9001 & Third-Party Audited: Facilities verified on-site by international inspection agencies including Bureau Veritas (BV), SGS, and TÜV Rheinland.
- CCPIT Certified Export Enterprise: Recognized member of the China Council for the Promotion of International Trade since 2005.
- Government Awarded Famous Brand: Honored as an Official Famous Export Brand with AAA-Grade Enterprise Credit Rating from the China Musical Instrument Association.
Frequently Asked Questions (B2B Procurement FAQ)
Detailed answers to critical commercial, manufacturing, and logistic queries for international OEM guitar importers.
Q: What is the Minimum Order Quantity (MOQ) for custom OEM guitar orders versus standard catalog items?
For standard factory catalog models (such as beginner cutaway acoustics or student electrics), our starting MOQs range from 1 to 10 pieces per model depending on existing inventory status. For full custom OEM private-label projects—including custom headstock shapes, proprietary body color lacquers, laser-etched laser branding, or customized retail packaging—the typical MOQ is 50 to 100 pieces per specification run, allowing flexible entry for growing brands.
Q: What OEM and ODM customization options do you support for guitar production lines?
We offer comprehensive private-label engineering. This includes sample-based cloning, 3D CAD design customization, headstock profile alteration, fretboard inlay routing, pickup voicing adjustments (custom humbucker/single-coil windings), hardware plating options (chrome, black nickel, gold, brushed bronze), finish types (satin, high-gloss, antique burst), and custom gig bag or hard-shell case branding.
Q: How does Chive Music manage CITES compliance and legal timber sourcing documentation?
All timber species utilized in our manufacturing facilities—such as maple, spruce, mahogany, basswood, and alternative fingerboard materials—are legally harvested and fully documented in strict compliance with international forestry laws. For orders utilizing restricted species governed by CITES regulations, our export department prepares all required phytosanitary certificates, chain-of-custody documentation, and re-export permits prior to vessel loading.
Q: What quality control standards and defect rate guarantees are provided?
Our factory operates under an ISO 9001 certified quality management framework. Every instrument undergoes a multi-point inspection covering structural integrity, finish smoothness, neck relief, electronics continuity, and acoustic tuning before packing. Our factory defect rate is maintained below 0.5%. In the event of transit or manufacturing defects, we provide free component replacement or credit reimbursement on subsequent orders.
Q: Can we consolidate different instrument categories in a single container shipment?
Yes, multi-category consolidation is one of our key enterprise advantages. As a unified manufacturing conglomerate supplying guitars, violins, cellos, brass instruments, woodwinds, percussion, and gig bags, buyers can consolidate diverse product lines into a single 20ft or 40ft High Cube container, dramatically lowering ocean freight cost per unit and simplifying customs clearing.
Q: What are the standard sample development and mass production lead times?
Custom pre-production sample evaluation models are typically completed within 15 to 25 days depending on specification complexity. Once samples receive client approval and mass production deposits are confirmed, standard factory lead times are 30 to 45 days for full container orders.
Request Our Comprehensive 2025 Wholesale Product Catalog
Access direct factory pricing, technical specifications, OEM customization blueprints, and minimum order guidelines across our complete instrument series.